
A Complete Breakdown for Investors and Industry Advisers
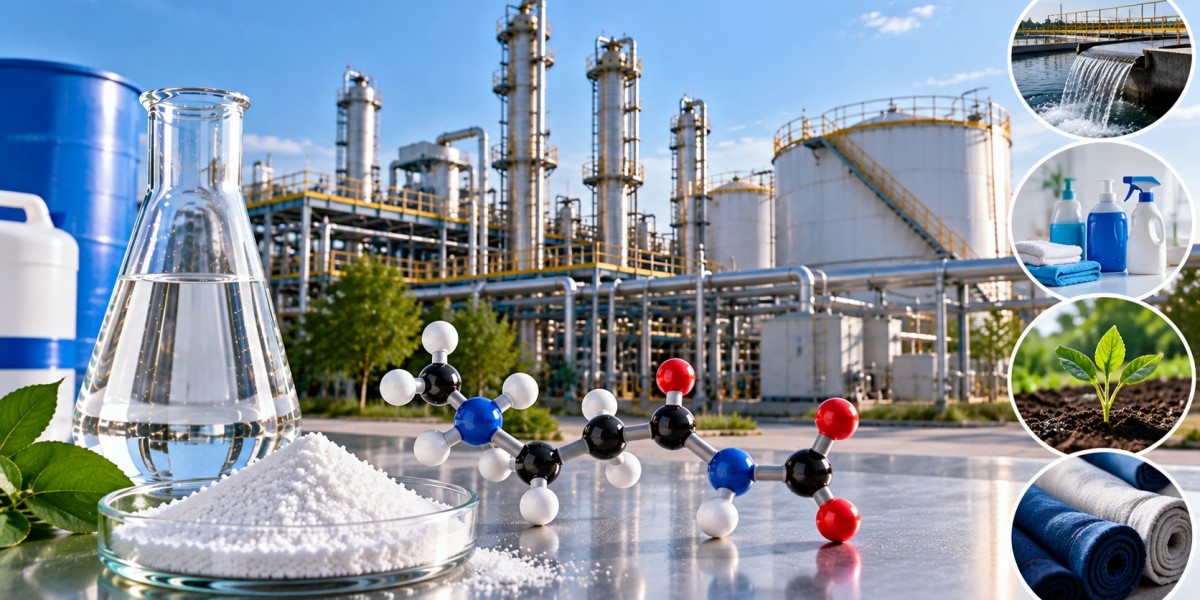
Anyone evaluating a specialty chemical manufacturing investment eventually runs into the same question: does the math actually hold up once you strip away the marketing gloss? For Ethylenediamine Tetra Acetic Acid, commonly known as EDTA, that question carries extra weight because the molecule feeds into water treatment, pharmaceuticals, food preservation, and cosmetics all at once. That breadth is a strength commercially, but it also means the cost structure is exposed to several unrelated feedstock and regulatory pressures simultaneously. That's exactly why a detailed Ethylenediamine Tetra Acetic Acid Production Cost Report matters so much to the people who have to sign off on capital before a single reactor gets built.
Investors, business brokers, corporate advisers, and finance companies rarely care about chelation chemistry for its own sake. What they care about is whether the numbers behind a plant hold together under real conditions: raw material price swings, energy costs, labor markets, environmental compliance, and financing terms. A production cost report translates the technical side of EDTA manufacturing into something a finance team can actually underwrite. Without it, you're essentially guessing at margins, and guessing with capital expenditure running into the tens of millions is not a strategy anyone should be comfortable with.
What a Production Cost Report Actually Covers
A well-built production cost report for EDTA isn't just a spreadsheet of raw material prices stitched together. It's a structured document that walks through every stage of turning basic feedstock into a saleable, food or pharma-grade chelating agent, pricing each stage out individually.
At minimum, it needs to cover the manufacturing process itself, since the specific route (acidification of an EDTA salt versus direct synthesis from ethylenediamine, formaldehyde, and sodium cyanide) changes yield, byproduct handling, and downstream purification requirements. It also has to account for raw materials and sourcing risk, utilities like steam and electricity, and the infrastructure needed to safely handle sodium cyanide, which is a genuinely hazardous input requiring strict containment and safety protocols.
Machinery costs, manpower requirements, packaging (EDTA typically ships as crystalline powder in multi-wall bags or as a liquid salt solution in drums), and transportation logistics round out the picture. A report that skips any one of these categories leaves an incomplete cost baseline, and incomplete baselines are how projects get approved on assumptions that fall apart the moment operations actually start.
Raw Materials Required for EDTA Production
EDTA synthesis depends on four primary raw materials: ethylenediamine, formaldehyde, sodium cyanide, and sulfuric acid, the last of which is used in the acidification step to convert the sodium or ammonium salt of EDTA into the free acid form. Ethylenediamine forms the nitrogen backbone of the molecule, and its price is closely tied to ethylene oxide and ammonia markets, both of which carry their own cyclical volatility.
Formaldehyde, produced via catalytic oxidation of methanol, adds another feedstock dependency, this one linked to methanol and natural gas pricing. Sodium cyanide is the trickiest input from a procurement and safety standpoint. It's tightly regulated, expensive to transport and store safely, and subject to supply constraints in many regions, which makes its availability a genuine risk factor rather than a routine line item. Any serious cost evaluation needs to treat sodium cyanide logistics as a distinct cost and risk category, not just fold it into general raw material spend.
Industrial Production Process for EDTA
The dominant industrial route synthesizes EDTA from ethylenediamine, formaldehyde, and sodium cyanide in a multi-step reaction, typically producing the tetrasodium or other salt form first. Ethylenediamine reacts with formaldehyde and sodium cyanide under controlled conditions to build up the four carboxymethyl groups around the nitrogen backbone, forming the EDTA salt as the primary product.
From there, the salt form can either be sold directly, since tetrasodium EDTA and similar salts have their own commercial markets, or it can go through an acidification step using sulfuric acid to convert it into the free acid form of EDTA. This acidification reaction precipitates the free acid, which is then filtered, washed, and dried to yield the crystalline product that most industrial buyers recognize. Why does the route matter so much? Because it changes both the capital equipment needed and the byproduct streams a plant has to manage, particularly around cyanide-containing waste, which carries its own disposal and regulatory cost burden.
Purification and crystallization at the tail end of the process determine final product purity, which matters enormously for pharmaceutical and food-grade applications where specification tolerances are tight.
Capital Investment and Plant Setup Cost Factors
Setting up an EDTA plant involves capital components that go well beyond a standard chemical reactor setup, largely because of the sodium cyanide handling requirement.
Land acquisition and site preparation come first, and costs here vary by region, but they're also shaped by proximity to feedstock suppliers and by local regulatory approval processes for handling cyanide-based chemistry, which can be lengthy and expensive in their own right. Equipment costs follow, covering the reaction vessels, filtration and crystallization systems, acidification units, and specialized containment and scrubbing systems required for cyanide safety compliance.
Engineering, procurement, and construction fees typically run as a percentage of total equipment cost, though EDTA plants often see this ratio pushed higher than average because of the additional safety engineering required around cyanide handling. Working capital requirements need careful sizing as well. Given that ethylenediamine, formaldehyde, and sodium cyanide prices can each move independently, a plant needs a cash buffer sized for multiple feedstocks moving unfavorably at once, not just one.
Operating Cost Factors
Once the plant is operational, the cost structure shifts from one-time capital outlays to recurring operating expenses, and this is where a detailed cost report genuinely earns its value for financial decision-makers.
Variable costs dominate, driven by the combined price of ethylenediamine, formaldehyde, sodium cyanide, and sulfuric acid, which together typically make up the largest share of total production cost. Utility consumption for the reaction, filtration, and drying stages adds meaningfully on top of that. Fixed costs cover labor, plant maintenance, insurance, and administrative overhead, and these tend to be more stable than raw material costs, though cyanide handling often pushes insurance premiums higher than a comparable non-cyanide chemical plant would face.
Labor costs vary by geography, and specialized safety training for cyanide handling adds a recurring cost that doesn't show up in more conventional chemical manufacturing. Maintenance costs need to account for corrosion and containment system upkeep specifically, since cyanide handling equipment often requires more frequent inspection cycles than standard process equipment. Financing costs and depreciation round things out, and the debt-to-equity structure a company chooses for the initial build materially affects effective cost per ton over the plant's operating life.
What Pushes EDTA Production Cost Up or Down
Several factors swing the numbers meaningfully, and understanding them genuinely helps before capital gets committed.
Feedstock pricing is the biggest lever, and because EDTA depends on three or four separate raw materials rather than one or two, its cost structure is more exposed to compounding volatility than many single-feedstock chemicals. Regulatory and safety compliance costs around sodium cyanide represent another major swing factor; regions with strict cyanide handling and transport regulations will see meaningfully higher compliance costs baked into the plant's fixed cost base.
Scale brings real advantages here too. Larger continuous-process plants spread fixed costs, including the substantial safety and compliance infrastructure, over greater output, which improves per-ton economics noticeably. Regional factors, including local energy prices, labor costs, environmental compliance requirements, and proximity to both feedstock suppliers and end-use customers in water treatment, food, and pharmaceutical industries, can shift total production cost by a wide margin between otherwise comparable plants built in different countries.
Frequently Asked Questions
Q: Why does sodium cyanide make EDTA production cost estimation harder than for most chemicals? Because cyanide isn't just a raw material cost, it's a regulatory and logistics cost too. Transport, storage, and handling regulations vary significantly by region, and a cost report has to account for compliance infrastructure separately from the actual cyanide purchase price.
Q: Is the acidified free-acid form of EDTA more expensive to produce than the salt forms like tetrasodium EDTA?
Generally yes, since acidification is an additional processing step requiring sulfuric acid and further purification. That said, the free acid form commands different pricing in food and pharmaceutical markets, so the extra processing cost often gets offset by higher realized selling prices.
Q: How much does regional regulation actually affect EDTA plant economics?
Quite significantly, honestly. Regions with strict cyanide handling laws or biodegradability concerns around EDTA's environmental persistence can add meaningful compliance costs, sometimes shifting overall production economics by well over 15 to 20 percent compared to more permissive jurisdictions.
Q: What's the most commonly underestimated cost in an EDTA project evaluation?
Working capital exposure across multiple feedstocks simultaneously. Because EDTA depends on ethylenediamine, formaldehyde, and sodium cyanide all moving independently, a plant needs a bigger cash cushion than a single-feedstock chemical process would require.
Q: Does downstream demand from cosmetics and food industries affect EDTA production cost planning?
Indirectly, yes. Demand shifts don't change the cost of making EDTA, but they do affect capacity utilization decisions, and a plant running below optimal utilization sees its fixed costs spread over less output, which raises effective cost per ton even if variable costs stay flat.
Why This Report Matters Before You Commit Capital
At the end of the day, a rigorous production cost report isn't a nice-to-have document, it's the difference between an informed investment decision and an expensive guess. For business brokers structuring a sale, for corporate advisers vetting a client's expansion plans, or for finance companies underwriting debt against a proposed EDTA plant, this kind of granular cost breakdown is what separates a defensible valuation from a speculative one.
The chemistry behind EDTA is well established and has been used industrially for decades. What changes constantly is the cost and regulatory environment surrounding it: feedstock prices across multiple inputs, cyanide handling regulations, energy markets, and regional labor availability. A thorough, up-to-date cost report accounts for all of that, and it gives decision-makers something they can actually stand behind when the capital is on the line.